Grain
The pore pattern of a hide is a fingerprint. It tightens along the back, opens across the belly, and no two animals wear it the same way. We grade for it rather than sand it away.

Demigod House Global Leather Export
Natural hides, slow tanning and the judgement of people who have read leather their whole working lives. Made in Kanpur, India, supplied to brands worldwide.
Where it begins
Born from nature, shaped by human hands. Our leather carries the character of its natural origin — every grain, every texture, every subtle imperfection telling its own story. From carefully sourced natural hides to the hands of skilled craftsmen, each piece moves through a slow, considered process where nature and human craft meet. The result is leather that feels authentic, ages beautifully, and becomes uniquely yours over time.
— The house standard, written down

Leather is skin. It carries the record of an animal's life — where it grazed, where it healed, where it grew. We grade that record honestly rather than sanding it away, because the marks are the proof the material is real.
The pore pattern of a hide is a fingerprint. It tightens along the back, opens across the belly, and no two animals wear it the same way. We grade for it rather than sand it away.
Fine parallel lines across the neck and shoulder — the record of an animal growing. On corrected leather they are buffed out. On full-grain we leave them, because they are the proof the surface is real.
A brush scratch, an insect bite, a fence. Skin repairs itself, and the repair stays visible. We cut around what would weaken a panel and keep what simply tells the truth.
Wax and oil leathers lighten where they bend and darken where they are handled. A year in, the piece has a map of its owner on it. That is not wear. That is the material finishing itself.
From field to finished hide
There is no shortcut through a hide. Tanning takes the time it takes, softening takes the time it takes, and every stage below is signed off by a person before the next one starts.
Hides arrive as a by-product of the food industry, bought from a closed list of suppliers with traceable, documented origin. Nothing enters the yard without provenance, and nothing is raised for its skin alone.
Each hide is opened, laid flat and read by hand for substance, marking and cutting yield. This is where character is separated from damage — and where a hide is matched to what it will eventually become.

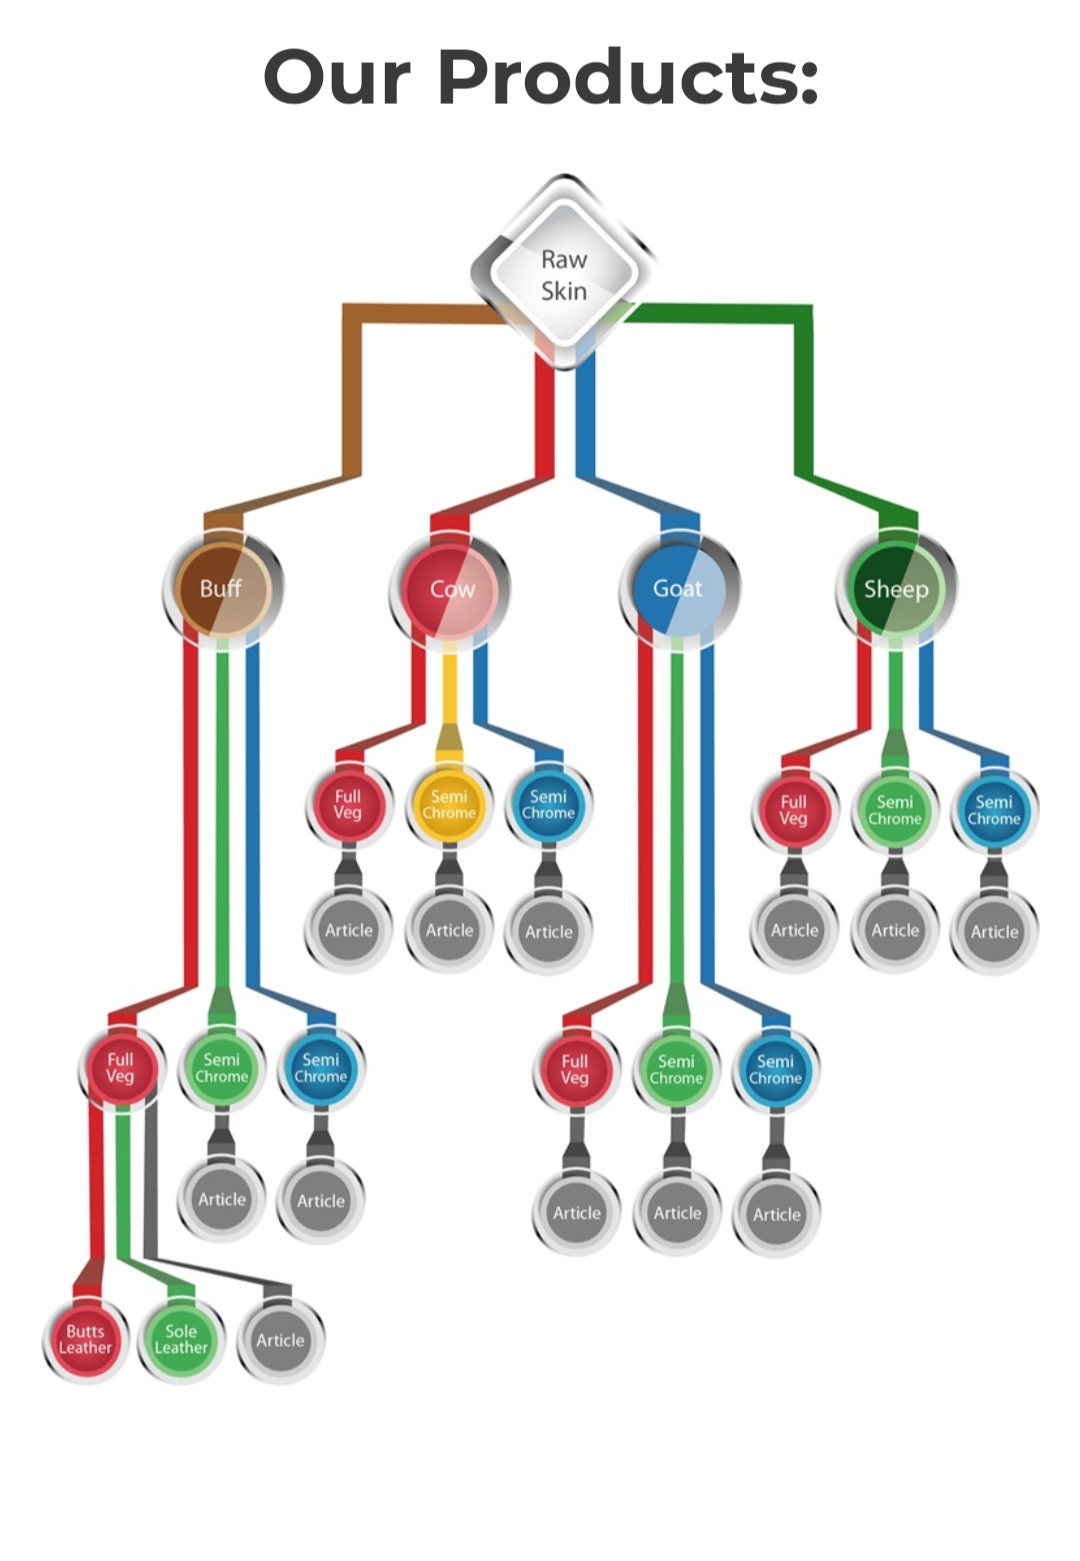
Chrome, vegetable and combination tanning in controlled drums and pits, with effluent treated on site before discharge. Vegetable tanning with bark extracts is the slowest route we offer, and the one that ages best.

Hours of tumbling relax the fibre until the hide breaks the way the design needs it to. Softness is not a setting; it is time, and the finisher decides when it has had enough.

Aniline dyes soak into the hide rather than sit on it, so the grain stays visible through the colour. Recipes are matched to your Pantone or your swatch, proved on a lab dip, and only then run at scale.

Wax, oil, foil, print, perforation, emboss. Some of it is machine work held to a tolerance; the burnishing and the hand-dyeing are exactly what they sound like — a person, a cloth and a judgement call.

Rub cycles, light fastness, tear strength, substance, colour consistency. The result is written down, signed, and travels with the goods. Nothing leaves the building on a verbal pass.
Rolled, laid flat or crated to survive the route, with documentation and certification coordinated in-house. FOB, CIF and DDP, to your port.

The people
Four judgements decide whether a hide is good, and none of them can be automated. A person opens it, a person watches the drum, a person decides when the surface has had enough, and a person signs the record that travels with your order.
Reads every hide at the yard by hand and eye before it is bought — substance, marking, symmetry, cutting yield. Roughly forty seconds a hide, thousands of hides a season, and a rejection here costs a fraction of a rejection at your cutting table.
Loads the drum, sets the float, watches the clock. Vegetable tanning in the pits takes weeks, not hours. There is no way to hurry it that does not show later.
Mills, stakes, dyes, coats and embosses — and decides, by feel, when a hide has had enough. Two hides from the same batch can need different time on the machine.
Signs the batch record. Substance, colour consistency, rub fastness, tear strength, yield. If it fails, you hear it from us before you find it yourself.
The house palette
Every colour below is a starting point, not a catalogue limit — recipes are matched to your Pantone or your swatch and proved on a lab dip before anything runs at scale.
Aniline · soft drape
Sanded · dry nap
Waxed · living pull-up
Coated · high reflect
Untouched · hair intact
Mirror · zero orange peel
Split · even pile
Pit-tanned · tools clean
Collections
From raw crust to a finished bag under your label. Each collection lists material, colourways, MOQ and what can be customised.
Full-grain and corrected-grain hides, tanned and finished to the tolerances that luxury manufacturing demands.
13 materialsHair-on cow and goat hides — the only material in our house where the animal writes the pattern.
6 materialsWhere the finishing department stops being a process and becomes a design studio.
8 materialsCut, stitched, edge-painted and packed under your label. Private label, OEM and ODM.
8 materials
Automotive, furniture and industrial materials — where the specification sheet matters as much as the hand.
8 materialsThe house
Demigod House Global Leather Export was founded in 2026. We say that plainly, because it is the point. No legacy processes to defend, no decades-old equipment to justify, no habits formed in a market that no longer exists — current machinery, a working colour laboratory, and a standard we set ourselves.
An initiative by Demigod House and Inland Leather Company.
To become the leather house international brands name in their specification documents — not because we are the largest, but because we are the most exact.
To make premium natural leather accessible to brands who refuse to compromise, through precise manufacturing, honest documentation and a genuinely short line between your designer and our finishing floor.
A material is not finished until it answers a brief. We start with what you are making and work backwards to the hide, rather than showing you what happens to be in the warehouse.
Machines hold the tolerance. People hold the standard. Every hide is read by hand at selection and again at inspection, and both readings are recorded.
Current equipment, a working colour laboratory, and a finishing team briefed to treat surface development as design rather than process.
Small first orders. Fast sampling. Direct contact with the people who actually make your material. No account layers between you and the floor.
Who we supply
Maisons and designer labels who specify a leather before they specify a season.
Multi-door retailers building private-label lines that have to hold their own beside the brands they stock.
Interior programmes where the material has to survive a test report before it survives a customer.
Studios and manufacturers working in large-format hide for seating and architectural surfaces.
Contract specification at volume — banquettes, headboards, casegoods and guest amenities.
Uppers, linings and soling supplied as a coordinated package to a single technical standard.
Structured leathers and hardware programmes for cases, trunks and travel goods.
Branded leather gifting produced to a house standard, with packaging to match.
Responsibility
Hides are a by-product of the food industry. Nothing is raised for its skin alone, nothing enters the yard without provenance, and the water leaves the site treated.
Hides are a by-product of the food industry, bought from a closed list of suppliers with traceable, documented origin. Nothing enters the yard without provenance.
Chrome and vegetable tanning run into on-site effluent treatment before discharge — to the standard our licence requires, and beyond it where we can.
Fair wages, safe conditions, no child labour, and an open door for client audit. We will host your compliance team on request.
Cutting plans are optimised for yield before production. Offcuts route to small goods and samples rather than to waste.
A growing share of our output is pit-tanned with bark extracts — slower, and considerably kinder to water systems than the alternative.
The most sustainable leather is the one that never needs replacing. We build for decades, and we test to prove it.
Our standard
“We will not ship what we would not accept.”
Every batch carries a documented inspection record — substance, colour consistency, rub fastness, tear strength, cutting yield. If a batch fails, you hear it from us before you find it yourself.
The Quality Commitment“Your specification is not a suggestion.”
Colour matched to Pantone or to a physical swatch, verified by lab dip before production. Substance and temper held to the tolerance you set, not the tolerance that is convenient.
The Specification Commitment“You talk to the people who make it.”
No account management layer. Your enquiry reaches the person who will run the batch. Questions answered within one working day, in writing, with a name attached.
The Access Commitment“We are new, and we will prove it on a sample.”
Founded in 2026, with nothing to coast on. Take a sample order. Judge us on the swatch, the lead time and the paperwork — then decide whether to give us the season.
The Founding Commitment


Questions
MOQ varies by material — typically 200–300 sq ft for finished leather, 20–30 hides for hair-on, and 50–200 pieces for finished goods. Each product lists its own MOQ. For first orders and sampling programmes we are flexible; tell us what you need and we will work to it.
Yes. We send a physical swatch card or sample piece for every material under consideration, and we build full prototypes for goods programmes before any production commitment. Sample lead time is typically 7–10 working days.
Yes. Send us a Pantone reference, a physical swatch, or a piece of the material you are currently using. Our finishing laboratory develops a matched recipe and returns a lab dip for approval before production begins.
Because it grew. Grain density, growth marks and healed scars differ across every animal and across a single hide. We grade and cut around genuine defects, but the variation you see in full-grain leather is the material telling the truth about where it came from. Corrected-grain and printed finishes are available where absolute uniformity is required.
All three. Private label applies your branding to our developed products. OEM builds to your technical pack. ODM starts from your brief and we handle design, pattern-making and development. Branding is applied in-house — embossing, debossing, foil, metal plates and custom packaging.
DHLE ships to Europe, the United Kingdom, North America, Scandinavia, the Gulf, Japan, Korea and Australia. We handle documentation, certification and freight coordination on FOB, CIF and DDP terms.
Every batch passes a documented inspection covering substance, colour consistency, rub fastness, tear strength and cutting yield. You receive the inspection record with the shipment. Nothing leaves the building on a verbal pass.
Finished leather: 21–30 days from order confirmation. Hair-on hide: 25–35 days subject to selection. Leather goods: 45–60 days including sampling. Repeat orders on an established specification run faster.
Because we were built for the market as it is now, not as it was thirty years ago. Our equipment, our testing protocols and our colour laboratory are current. We compete on precision, responsiveness and documentation — and we will prove all three on a sample order before you commit to anything.